Leave Your Message
Discover our top-performing food-grade solutions engineered for retail display, freshness preservation, and convenient takeaway performance.
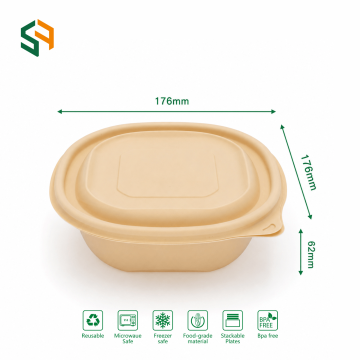
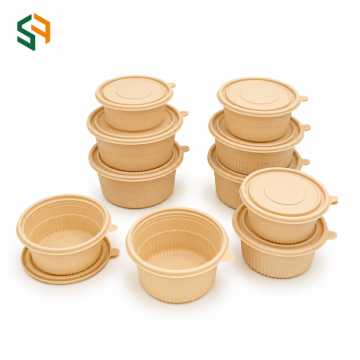
The global retail landscape is witnessing an unprecedented shift in consumer dining behaviors. Supermarket deli counters and pre-packaged ready-to-eat (RTE) meals have transformed from simple convenience options into core revenue drivers for major grocery chains. With busy modern lifestyles, consumers demand fresh, high-quality, and portion-controlled meals that require minimal preparation. This shift has placed plastic tray food packaging at the absolute center of retail food logistics and merchandising strategies.
Today's supermarkets are no longer just grocery stores; they are hybrid food service providers. The deli department requires packaging that can withstand rapid temperature transitions—from blast freezing and cold storage to microwave heating and high-temperature heat lamps. Consequently, plastic trays have evolved from mere storage containers into highly engineered components that actively preserve food quality, extend shelf-life, and establish brand identity on crowded retail shelves.
Analyzing how specialized plastic tray food packaging solves unique challenges across diverse retail and industrial food sectors.
Hot deli counters require materials that remain structurally sound under intense heat. Standard polypropylene (PP) trays are the industry benchmark here, offering thermal stability up to 120°C (248°F). These trays hold hot entrees, gravies, and roasted meats under warming lamps without warping, softening, or releasing chemical contaminants into the food.
For chilled or frozen pre-packaged meals, dual-ovenable or microwave-safe plastic trays are essential. Dual-compartment and multi-compartment layouts keep main dishes and side elements separate, preventing flavor migration and maintaining texture. Leak-proof sealing rims allow for hermetic film sealing, preserving freshness during distribution.
To extend shelf life without chemical preservatives, supermarkets utilize Modified Atmosphere Packaging (MAP). High-barrier plastic trays (often combining PP with EVOH barrier layers) restrict gas transmission. This keeps red meats red, salad greens crisp, and prepared pasta fresh for up to three times longer than standard packaging.

The plastic packaging industry is undergoing a massive technological revolution. The modern supermarket deli sector is balancing the critical need for food safety and shelf-life extension with growing environmental responsibilities. As a result, the development of sustainable, bio-based, and highly recyclable plastic food trays has accelerated rapidly.
Corn Starch-Based Bioplastics: Biodegradable and compostable alternatives are gaining significant traction for dry, cold, or short-shelf-life deli items. By blending natural corn starch with biodegradable polymers, manufacturers produce rigid trays that dramatically reduce carbon footprints while maintaining the required structural integrity.
Mono-Material Recyclability: Historically, multi-layer trays were difficult to recycle. The current trend focuses on mono-material PP or PET structures that deliver high gas-barrier properties through ultra-thin coatings, ensuring the entire tray can be easily processed in standard municipal recycling streams.
Professional Food Packaging Solutions Provider specializing in the production of disposable and recyclable food containers.
With 20 years of industry expertise, we are a professional manufacturer focused on the R&D and production of food packaging containers.
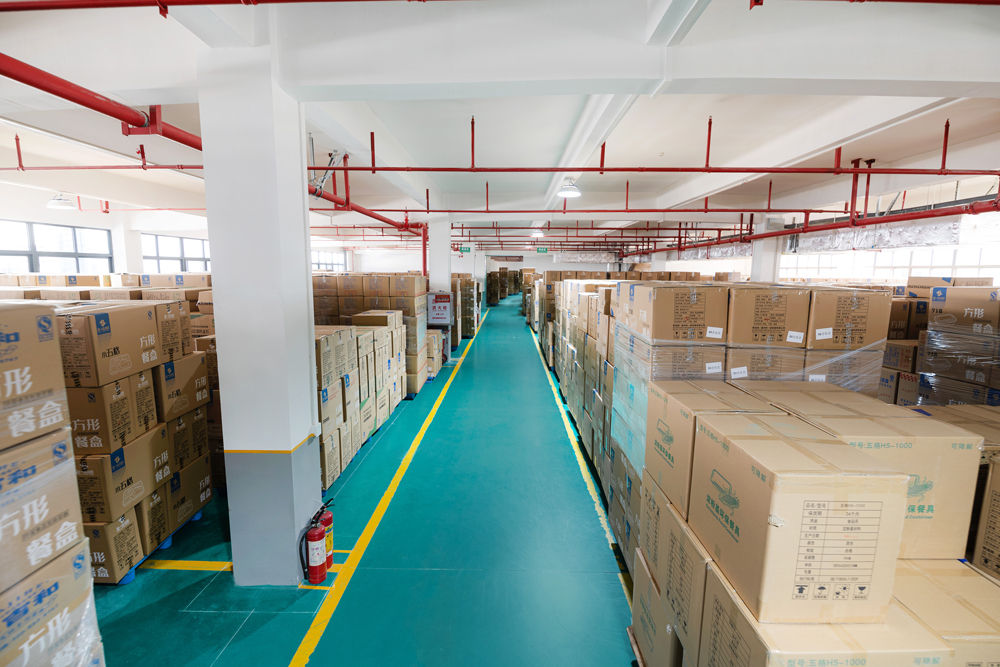
Located in Fuzhou City, Fujian Province, China, we own an 18,000m² modern production base equipped with high-standard clean workshops and over 50 automated production lines, supported by a professional team of more than 100 members.
Backed by our fully integrated production system covering the entire process from raw materials to finished products, we deliver comprehensive control over quality and efficiency across every stage of manufacturing.
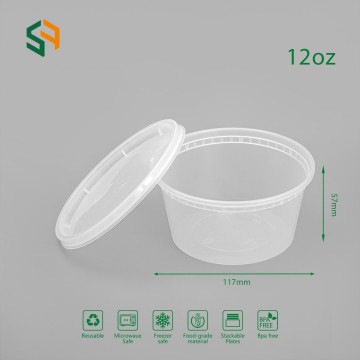
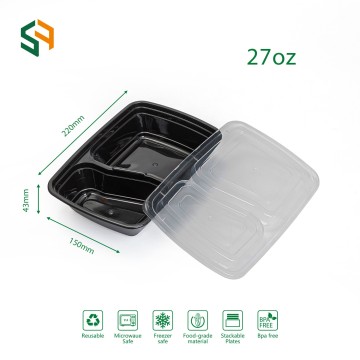
To meet the diverse demands of global supermarkets, hypermarkets, and industrial food packaging lines, we offer an extensive range of specialized product series:

We combine advanced polymer chemistry with high-precision thermoforming technology to deliver superior retail packaging performance.
Our trays feature engineered structural ribbing to prevent crushing during stacking, precise sealing flanges to eliminate leaks, and crystal-clear material clarity to showcase your culinary creations beautifully.
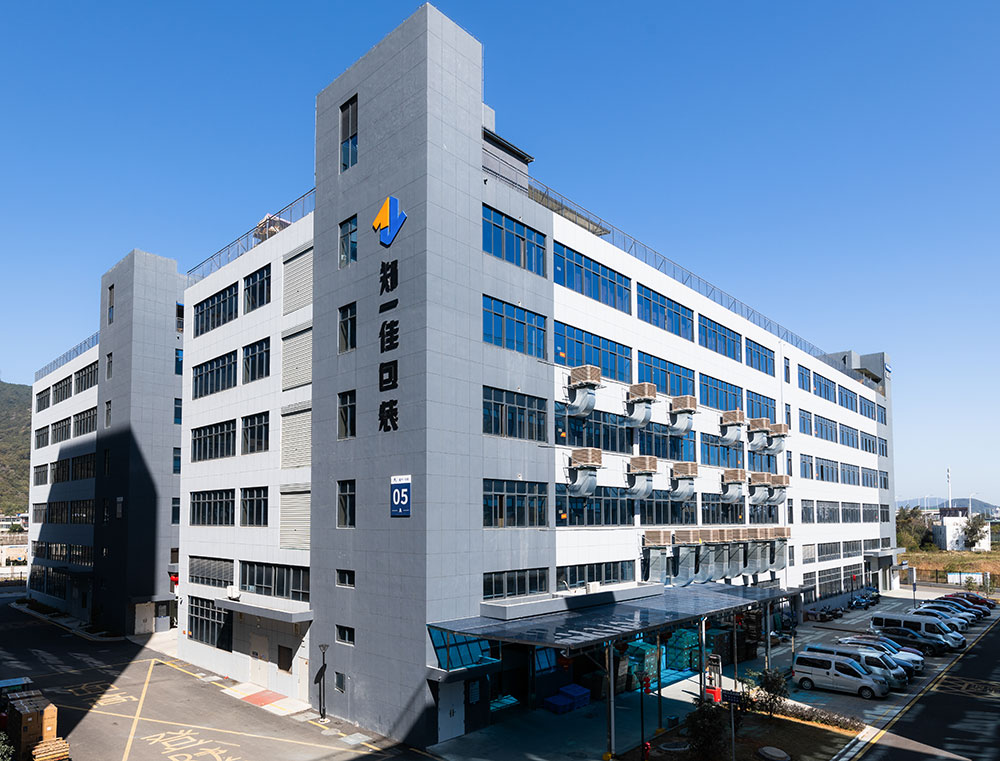
With over 100 in-house mold systems, we respond quickly to your custom needs and deliver end-to-end packaging solutions. Committed to exceptional value and uncompromising quality, we directly enhance your customers' satisfaction and strengthen your market position.
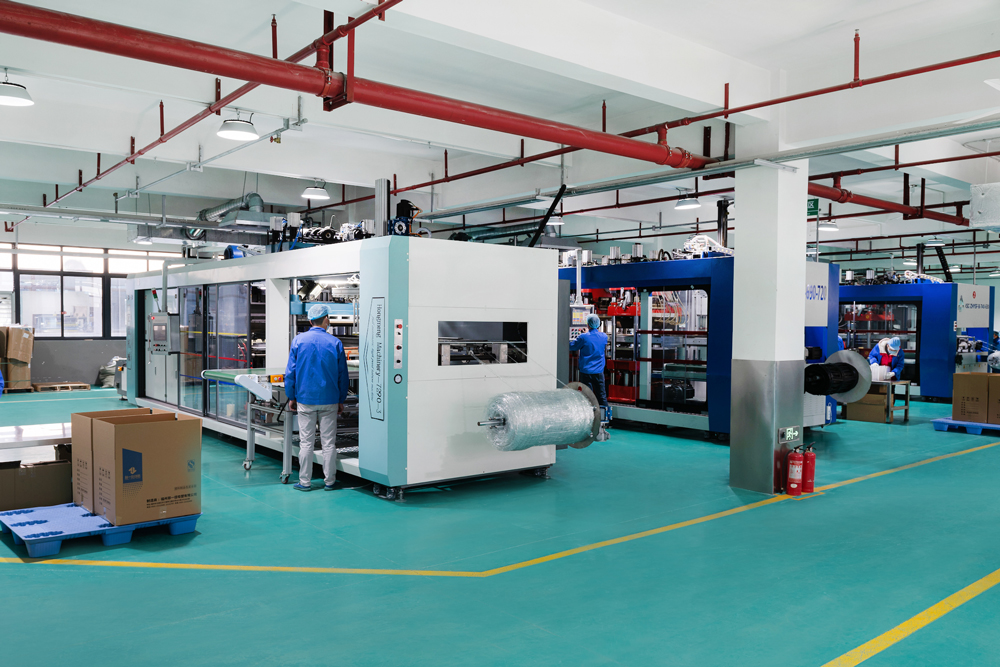
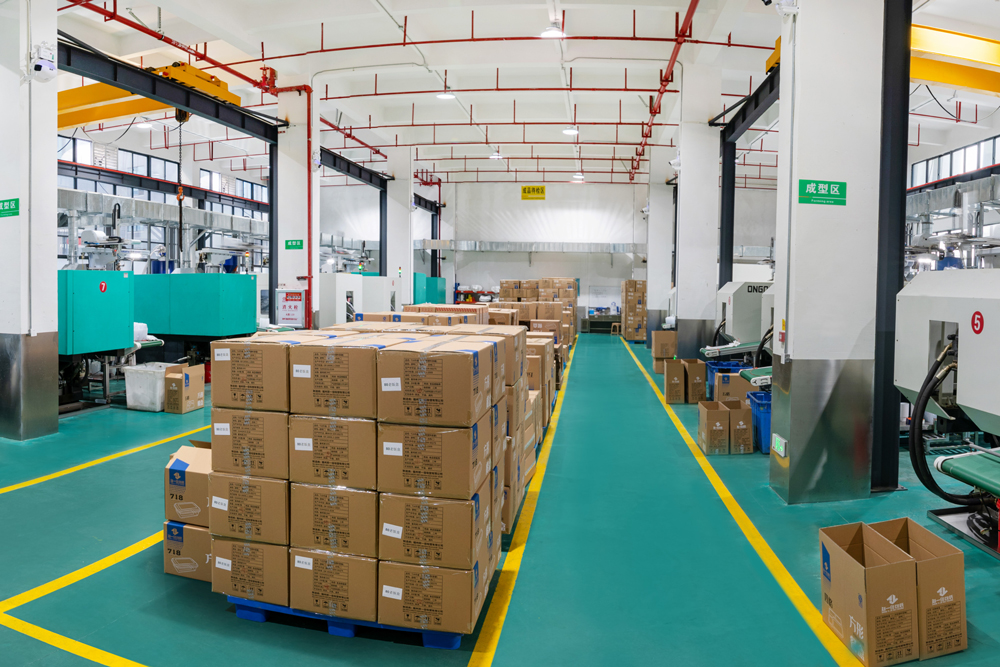
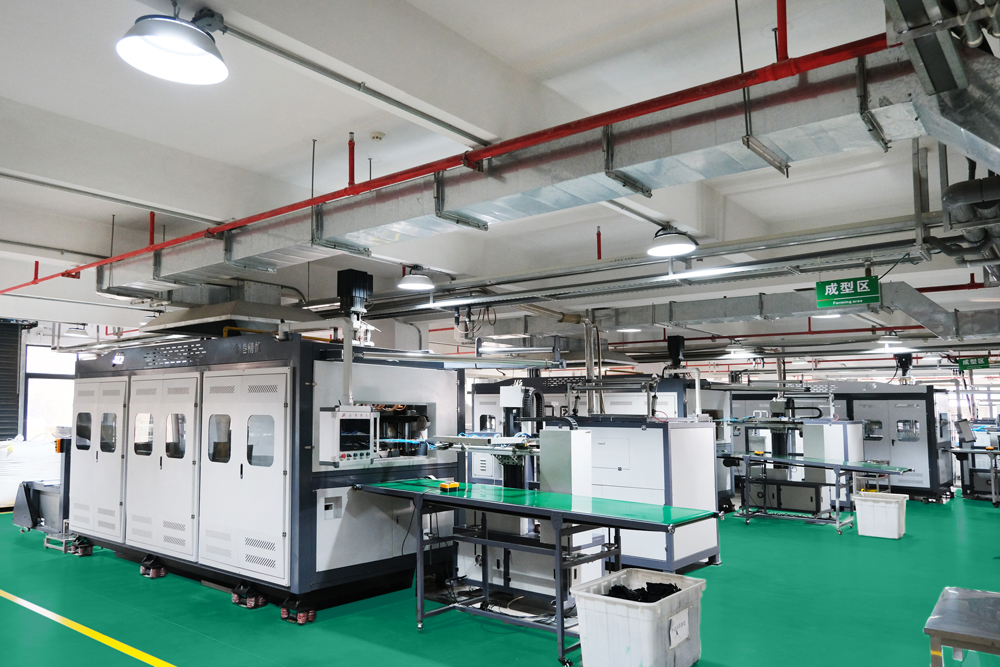
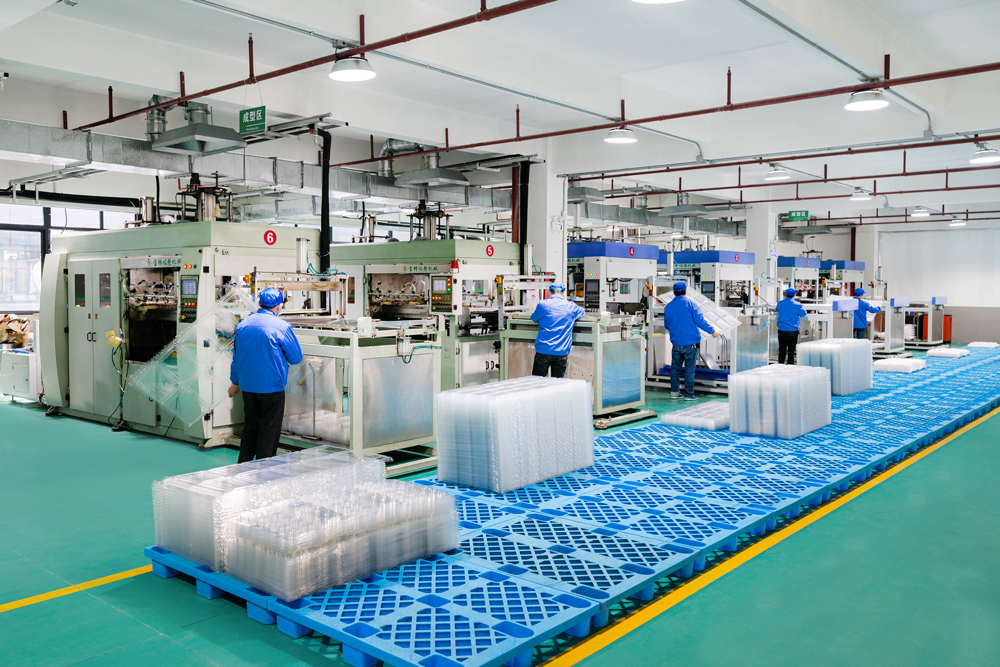
Our Fuzhou-based manufacturing plant runs state-of-the-art multi-station thermoforming machines that integrate sheet extrusion, forming, cutting, and stacking into a single continuous process. This high level of automation guarantees absolute dimensional consistency, which is critical for automated de-nesting and high-speed filling lines used by industrial food packers.
We are certified to ISO9001, ISO14001, HACCP, and QS for food-grade packaging. By combining our in-house CNC mold technology with strict quality control, we ensure the safety, stability, and reliability of every product.
Our forward-looking approach, reliable quality, and competitive pricing have earned long-term trust from global customers. With years of experience, we deliver high-quality products; through continuous innovation, we drive sustainable development. We are committed to healthy lifestyles and a greener future with sustainable packaging solutions.
Every batch of raw plastic resin (PP, PET, PS, or PLA) undergoes strict inspection for purity, food-grade certification, and heavy metal compliance before entering our production lines.
Our finished packaging trays are tested for load-bearing capacity, impact resistance at low temperatures, and seal integrity, ensuring they perform flawlessly throughout the supply chain.
Browse our complete collection of industry-proven food containers, designed for maximum freshness, safety, and shelf appeal.